 English
 中文
 Sep 19,2026
Article Overview: This guide explains juxin machinery capacity for procurement managers, sourcing teams, and project engineers preparing to buy rigid box making, case making, and auxiliary equipment. It covers what buyers should define before purchase, how to evaluate supplier capacity statements, and what evidence should accompany a quotation. The conclusion is that capacity should be agreed as a measured production envelope under named sample and shift conditions, not accepted as a headline speed. Evidence boundary: no verified equipment specifications were supplied for this page, so all figures must be confirmed per model and quotation.
What Should Buyers Know About Juxin Machinery Capacity?
Buyers should treat juxin machinery capacity as a conditional production envelope, not a single number: it depends on box format, material, shift pattern, automation level, and operator skill, and must be confirmed in writing against your own samples.
Capacity statements describe different things. Rated capacity is the figure published for a defined format and material at stated conditions. Demonstrated capacity is what a machine actually produces during a witnessed trial. Sustainable capacity is what remains once changeovers, material feed interruptions, maintenance windows, and operator breaks are included. Each is legitimate; mixing them is a common source of disputes after installation. Ask the supplier to label every number with the condition set it assumes.
For rigid box and case making equipment, capacity is rarely one figure across a product family. Lid and base boxes, wrapped rigid boxes, and specialty formats involve different operation sequences, and each added step introduces its own cycle time and failure modes. Buyers therefore need a demand profile with realistic format percentages rather than a single annual box count.
A careful buyer treats any quoted capacity as a hypothesis to be tested. Define the sample formats that represent the bulk of your volume, require a witness trial on those samples, and record the results. That converts a supplier figure into a measurable acceptance criterion that can be written into a purchase order.
Operating Requirements That Define the Production Envelope
The production envelope is the set of input conditions under which a stated capacity holds. Write it down before comparing suppliers, because a capacity figure without its envelope cannot be verified.
- Box footprint and depth
- Minimum and maximum board length, width, and box height the format range must cover.
- Board and wrap materials
- Greyboard grades and thicknesses, wrap paper weight and finish, and any laminated or specialty stock.
- Adhesive and drying behaviour
- Whether the glue system and drying time constrain line speed on your materials.
- Annual volume and order pattern
- Total boxes, average and peak order size, seasonality, and changeovers per shift.
- Shift pattern and staffing
- Working hours per year, operator count, and the skill level assumed for feeding and inspection.
- Utilities and floor conditions
- Power supply, compressed air, and the space needed for loading and unloading.
These inputs feed a simple capacity relationship that buyers can use for planning. For illustration, take a hypothetical planning case:
C = (H × η) / t
where C is good-unit capacity in units per year, H is planned productive hours per year, η is the fraction of those hours actually producing good units, and t is the effective cycle time per unit in hours. If t is measured in seconds, use C = (H × 3600 × η) / t. The relationship is only as good as its inputs: η combines availability, performance, and quality losses, so use a measured value from a trial or from comparable equipment you already operate. The numeric values in this illustration are hypothetical; treat calculated output as a planning estimate rather than a contractual commitment.
Uptime assumptions deserve scrutiny because they influence usable capacity more than peak speed does. Planned maintenance intervals and spares availability belong in the negotiation, and the rigid box making machine maintenance guide outlines how service routines affect long-run availability. Ask how preventive maintenance windows are scheduled and what response time applies to unplanned stoppages.
Configuration and Automation Trade-Offs
Automation decisions change capacity in ways a speed comparison does not capture. Consider a hypothetical mixed-format scenario: a semi-automatic configuration may reach a similar cycle time on one stable format while requiring more operators and more manual handling between steps. A fully automatic line typically reduces labour per box and stabilises quality, but it also increases changeover complexity and the cost of any stoppage.
Three trade-offs usually decide the configuration:
- Labour versus flexibility: manual feeding and positioning absorb format variation, while automated handling demands tighter incoming material tolerances.
- Changeover time versus run length: automation pays back on long runs, but when average orders are short, setup and changeover dominate the working day.
- Buffer and accumulation: without buffers between stations, the slowest station sets line capacity, and any upstream stop propagates immediately.
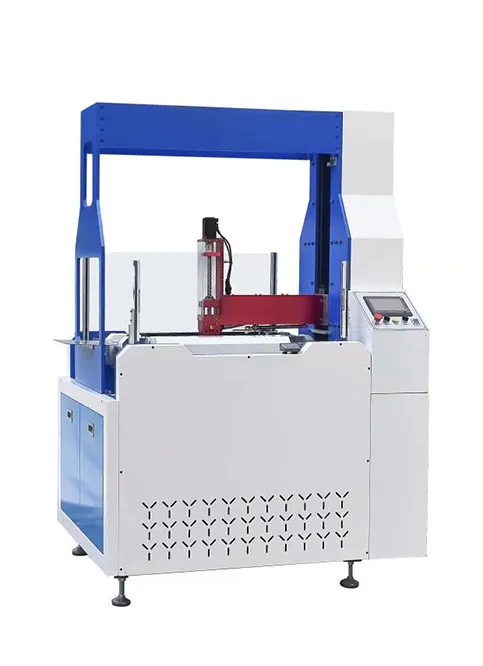
Auxiliary equipment belongs in the same calculation. If the product mix includes magnetic closures, an automatic magnet and steel sheet pasting machine adds a step with its own cycle time and quality checks, so its output has to be matched to the main line instead of assumed to follow it. The same logic applies to corner pasting, gluing, and slitting stations.
How Should Teams Evaluate Juxin Machinery Capacity in an RFQ?
Teams should evaluate juxin machinery capacity by defining sample formats, requesting a written cycle-time basis, testing the same samples, and tying payment milestones to the measured results of factory acceptance tests.
Step 1: Define the demand profile in writing
Attach format drawings, board and wrap specifications, annual volumes, order-size distribution, and shift pattern. Note which formats are must-run and which are occasional.
Step 2: Request a capacity statement with its basis
Ask for cycle time or output per operation, the sample specification used, the shift pattern assumed, and whether changeovers, cleaning, and breaks are included. A number without this basis cannot be compared across suppliers.
Step 3: Run a witnessed trial on representative samples
Send materials you would use in normal production, not hand-selected samples. Record output, rejection reasons, operator interventions, and stoppages over a defined period rather than a short burst.
Step 4: Convert the trial into acceptance and commercial terms
Write the tested conditions and the measured result into the acceptance criteria, then tie payment milestones and warranty wording to them. Confirm spares, training, installation support, and response times in the same document.
Timing should be verified rather than assumed. Juxin Machinery's published FAQ states a freight preparation period of 7–15 days, with some combination machines taking 30–45 days; treat those as supplier-stated planning inputs and confirm them for your configuration and destination. The same source lists installation guidance, user training, and maintenance support among after-sales services, which are reasonable items to define in scope and duration before signing.
What Evidence Is Required for Juxin Machinery Capacity?
Evidence should include a written cycle-time basis with assumed sample specifications, a factory acceptance test on your samples, measured output over a full shift, maintenance and spares data, and a documented quality inspection routine.
- A written capacity statement naming the sample specification, shift pattern, and inclusion or exclusion of changeover and downtime.
- Cycle-time data per operation for each must-run format, including the slowest station in the line.
- Trial records from production-representative materials, with output, rejects, and stoppage reasons.
- Quality inspection and calibration routine, and how non-conforming output is handled.
- Maintenance intervals, recommended spares list, and stated response time for support requests.
- Training and installation scope, including who provides materials and who signs off acceptance.
Visual evidence helps validate what a written statement claims. Recorded run footage on formats similar to yours is a practical starting point, and the video library covering Juxin Machinery equipment can be reviewed before a factory visit or a witness trial. Use recordings to prepare questions, not as a substitute for measured results on your own samples.
Where a claim cannot be verified, ask for the condition set behind it or exclude it from the decision. A capacity figure that a supplier will not qualify in writing should not carry weight in a supplier comparison.
FAQ
How many machines does a given annual output require?
Divide annual good-unit demand by the sustainable capacity per machine at your shift pattern, then add margin for seasonality and maintenance. If the total exceeds one line, the split between machines usually follows format families rather than volume alone. Run the calculation with measured cycle times, not catalogue figures, before committing to a configuration.
Should capacity be verified before or after the purchase order?
Verify on representative samples before the order is placed, and again at factory acceptance testing before shipment. Pre-order trials influence configuration and price; acceptance testing protects the payment milestone. If a pre-order trial is not possible, define the acceptance test in the contract so a shortfall has a defined remedy instead of becoming a negotiation after delivery.
Which auxiliary equipment affects the production envelope?
Any station that adds an operation to the box: corner pasting, gluing, sheet or magnet pasting, slitting, and inspection points. Each has its own cycle time and tolerance limits, so line capacity is set by the slowest stage unless buffers are included. Map the full process sequence and list the cycle time for every step before comparing configurations.
How should buyers interpret delivery and installation statements?
Treat published lead times as planning inputs and confirm them for the exact configuration, destination, and shipping method. Ask for a milestone schedule covering production, inspection, shipment, installation, and operator training. Because installation and training consume capacity during ramp-up, include that period in your own output plan rather than assuming full output from the first week.
Conclusion: Buying Capacity as a Defined Envelope
Juxin Machinery capacity is defined by a conditional production envelope rather than a single headline figure. Buyers who document format ranges, materials, volumes, and shift patterns first, then request a qualified capacity statement and verify it on their own samples, have a clearer basis for comparing suppliers and for protecting the investment after installation.
The sequence is consistent: document requirements, request the basis behind every number, test on production-representative materials, convert results into acceptance criteria, and confirm maintenance, spares, and training scope. A configuration consultation should start from that demand profile, because measurable inputs can be compared and verified, while a single box count cannot.